
Flow control systems are important to all industrial processes in ensuring efficiency, safety, and reliability. Whether it is a refinery plant or any other industry, there are always valves employed in order to facilitate the passage of either liquids or gasses. Among the most common types of industrial valves include gate valves, globe valves, and knife edge valves, among others.
Selecting dependable industrial valves should be done by working with reputable industrial valve manufacturers. One such company is Metflow Engineers which has made its name as a leading supplier of industrial valves.
The Role of Gate Valves in Industrial Processes
Among the various types of valves used in industrial systems are gate valves. These are the valves that are normally employed when it comes to isolating fluid pipelines in industrial systems. They offer unrestricted passage when fully open and also total shut-off when closed.
Benefits of Gate Valves
• Unrestricted flow when open
• Sealing capability
• Durable
• Pressure tolerant
• Low maintenance requirements
• Highly reliable
Due to these benefits, industries continue to rely on gate valves.
Importance of Quality in Valve Selection
The industrial setting usually requires valves that function within extreme conditions of temperature, pressure, and harsh medium along with being in operation throughout. Using low-quality valves in such situations would mean leakage, machine failure, high maintenance, and even safety threats.
Hence, quality valve manufacturers offer:
• Quality products
• Product conformation to industry standards
• Reliability over time
• Decreased maintenance cost
• Improved workplace safety
That is why businesses in any industry opt for Metflow Engineers as their go-to solution provider for state-of-the-art valves for their needs.
Metflow Engineers: Valve Manufacturing by the Experts
Metflow Engineers is recognized for their industrial valve production through which they offer customers durable, efficient and precise valves that will serve your business well. With a high quality commitment, Metflow Engineers offers innovative and quality valves to its valued customers.
Some Key Features of Metflow Engineers Valves:
• Precision engineered
• Leak-proof seal
• Corrosion resistant
• Capable of high-pressure operations
• Smooth performance
• Durability
These features ensure efficient industrial operations without any downtime and costly maintenance.
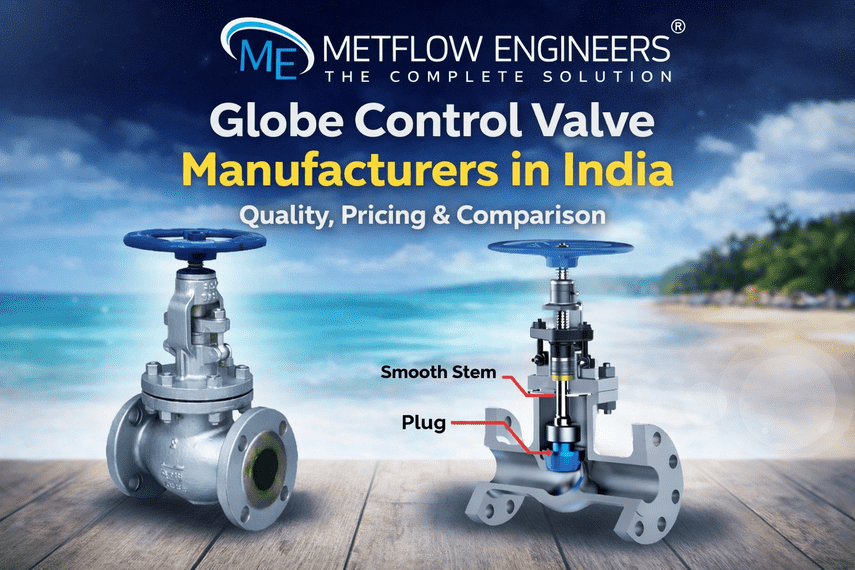
Supplier of Globe Valves for Exact Process Control
Although gate valves are mainly used for shutting purposes only but there comes situations in which flow control and throttling is required in addition to flow shut-off.
For these purposes, globe valves are used, which makes Metflow Engineers a popular choice amongst businesses. If you’re looking for globe valve supplier, then Metflow Engineer is the best choice.
Advantages of Globe Valves
• High throttling ability
• Accurate flow regulation
• High shut-off ability
• Efficient pressure regulation
• Able to withstand high temperatures
• Sectors Using Globe Valves
• Thermal Power Plants
• Chemical Industry
• Pharmaceutical Industry
• Oil and Gas Industry
• Steam distribution system
There is a need for globe valve manufacturers who provide reliable and effective valves for their processes.
Knife Edge Valve Solution for Specific Industrial Processes
In some cases, an industry might be processing corrosive slurries, thick liquids, and solid material-containing liquids which might not be handled easily by valves. For such cases, a knife edge valve is recommended.
A knife edge valve is specially designed to cut through viscous and thick liquid with suspended particles.
Advantages of Knife Edge Valves
• Handling of slurries
• Proper shut-off
• No risks of clogging
• Sturdy design
• Ability to handle harsh conditions
• Low maintenance
Applications of Knife Edge Valves
• Mining Industries
• Pulp and Paper Industries
• Water treatment plants
• Cement production facilities
• Chemical Industry
• Power stations
At Metflow Engineers, we manufacture tough knife edge valves that work effectively in demanding industries.
Application of Advanced Valve Systems in Industries
Modern industries require advanced valve technology in order to operate and achieve safety requirements.
• Oil and Gas Sector
• Pipeline isolation and control
• Water Treatment Plants
High-quality valves control the distribution of water, filtration process, and proper management of wastewater.
Chemical Processing
These valves allow controlling the process involving dangerous, aggressive chemicals and other corrosive substances.
Power Generation
These valves help in regulating processes within steam systems, cooling, and utilities network.
Manufacturing Facilities
Flow control systems help manage equipment operations.
The versatile usage of gate valves, globe valves, and knife edge valves made them valuable for many industries.
Why Companies Need to Partner with Metflow Engineers
Advanced Production Methods
Metflow Engineers maintains advanced manufacturing plants to make the production process smooth and ensure quality.
Skilled Engineering Staff
The skilled engineering staff at Metflow Engineers ensures innovation through their expertise.
Quality Assurance Process
Every product is subject to rigorous testing before delivery.
Customized Solutions
Metflow Engineers creates customized solutions for every project requirement.Customer Focus
Metflow Engineers prioritizes customers' satisfaction through efficient and professional services.
Conclusion
Proper control over the process of water flow helps businesses operate efficiently. The selection of proper gate valve supplier in india and gate valve providers of globe valves is important. Metflow Engineers helps clients find the best knife edge valves for abrasive media.
Metflow Engineers produces a wide range of valve products designed to provide businesses with the highest quality valves. It uses innovation and experience to offer high-performance solutions to all its customers.
Metflow Engineers is the reliable partner in search for industrial flow control valves.